


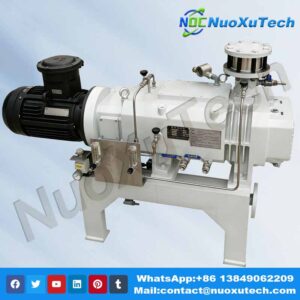

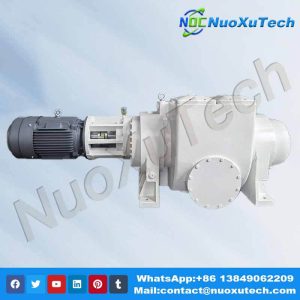
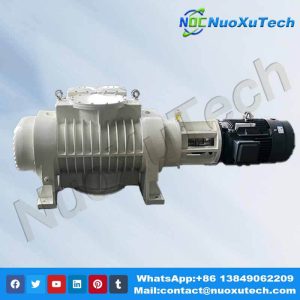

Application of Vacuum Technology in the Food and Beverage Industry, The food and beverage industry continually seeks innovations to enhance product quality, extend shelf life, and optimize production efficiency. One such transformative solution is vacuum technology. From packaging to sterilization and specialized processing, vacuum pumps play a crucial role in improving operations. By leveraging vacuum solutions, manufacturers can ensure superior product outcomes while meeting consumer demands for quality and safety.

Vacuum Technology in Food Packaging
A significant application of vacuum technology in the food and beverage industry is in packaging. Vacuum pumps remove air from food packages, reducing oxidation and preventing spoilage. This method extends the shelf life of products and preserves their taste and quality. By eliminating odors, vacuum packaging ensures fresh and odor-free products reach consumers.

Degassing in Mineral Water Production
Mineral water naturally contains carbonic acid, minerals, and iron. When exposed to air, dissolved iron oxidizes, negatively impacting the water’s taste. With vacuum technology, carbonic acid is removed at pressures as low as 50 mbar. This process not only preserves the quality of the water but also prepares it for the production of carbonated beverages like soda water.
Deodorization of Oils and Fats
Exposure to air can cause salad oils and fats to develop unpleasant odors. To address this, steam is introduced to absorb the odors. A vacuum pump then extracts the steam, leaving the oils and fats odor-free and ready for further processing. This application of vacuum technology is essential in maintaining the flavor and quality of edible oils.
Salmon Processing with Vacuum Systems
High-speed salmon processing utilizes vacuum technology to streamline operations. In automated systems, vacuum pumps efficiently remove waste materials, including brine, fat, protein, and residual fish parts. This technology enables rapid cleaning, processing each salmon in just three seconds, ensuring high productivity and cleanliness.
Sterilizing Tea and Spices
Tea and spices transported from tropical regions often carry pests, bacteria, and fungi. Before further processing, these contaminants must be eliminated. By employing vacuum technology, the air is evacuated from containers, creating a sterile environment. Subsequently, steam or germicidal gases are introduced to ensure the complete removal of harmful microorganisms.
Improving Sausage Production
Vacuum technology plays a pivotal role in sausage manufacturing. During the mixing process, vacuum pumps remove air to prevent oxidation, which can adversely affect the taste, color, and texture of the final product. By maintaining a pressure of approximately 100 mbar, vacuum pumps ensure that the sausages retain their quality and visual appeal.
Accelerating Ham Soaking Processes
Traditional ham curing methods are increasingly being replaced by vacuum soaking techniques. By evacuating air, vacuum pumps speed up the soaking process, allowing flavors and curing agents to penetrate the meat more effectively. This modern application of vacuum technology ensures consistent quality in ham production.
Humidification of Tobacco Products
Tobacco products require proper humidification to maintain their integrity during processing. Without adequate moisture, the tobacco becomes brittle and prone to breakage. Vacuum pumps create a controlled environment by removing air from packaging, followed by the introduction of steam and, occasionally, fragrances. This application of vacuum technology ensures the durability and quality of tobacco products.
Vacuum Evaporators in Liquid Processing
Liquid ring vacuum pumps are integral to evaporation processes in the food and beverage industry. These systems assist in separating liquids from mixtures, enhancing efficiency in various applications, such as:
- Milk evaporators in dairy processing
- Thick liquid evaporators in pulp mills
- Crystallizers in chemical manufacturing
- Tray evaporators in sugar refining
Depending on operational needs, these vacuum pumps are available in standard or stainless steel configurations, offering reliability and durability.

The application of vacuum technology in the food and beverage industry has revolutionized manufacturing processes, enhancing efficiency, safety, and product quality. From extending shelf life through vacuum packaging to optimizing complex production tasks, vacuum pumps provide unmatched versatility. By adopting these advanced solutions, manufacturers can meet the growing demands of the global market while maintaining exceptional standards of quality and sustainability.
Contact Us
For more information about the “Application of Vacuum Technology in the Food and Beverage Industry” contact Nuoxutech at contact@nuoxutech.com or visit our Blogger nuoxutech.blogspot.com .You can also reach us on WhatsApp at +86 13849062209.Our team is ready to provide you with professional service and support.
Keywords:
vacuum technology in the food and beverage, vacuum packaging, Vacuum Technology in the Food and Beverage, vacuum pumps,vacuum system, liquid ring vacuum pump, 2bec, Vacuum Technology in the Food and Beverage, food and beverage processing, Vacuum Systems in Food Packaging, Nuoxutech, Vacuum Applications in Beverage Industry, China-made vacuum systems for food freeze drying degassing and concentration